Faça o seu trabalho de forma eficiente!




Common fabrication mistakes in stone processing often begin long before the cutting machine starts. Inaccurate measurements, poor slab inspection, incorrect cutting layouts, unsuitable tools, weak slab support, machine calibration problems, unsafe material handling, and insufficient quality control can all create serious stone cutting errors. A reliable fabrication system should control the entire workflow from slab storage and project measurement to cutting, inspection, handling, packaging, and final delivery.
Common Fabrication Mistakes in Stone Processing: 18 Errors to Avoid
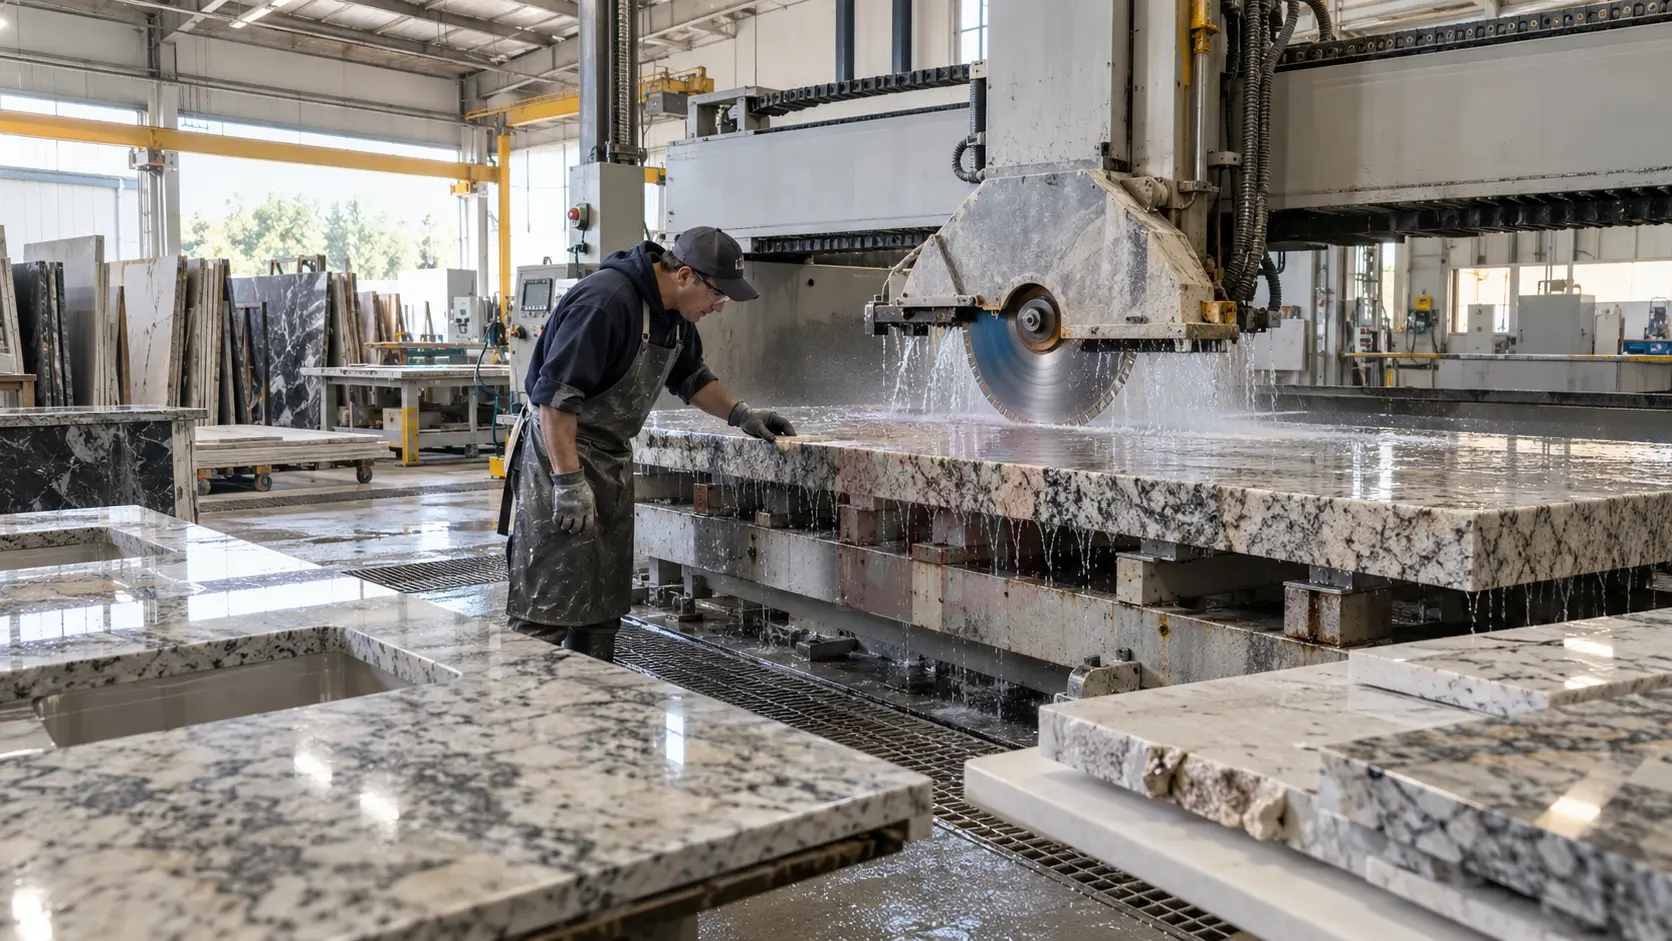
Common fabrication mistakes and stone cutting errors in a professional stone workshop
Even experienced stone fabrication shops can lose valuable material, production time, and labor because of avoidable fabrication mistakes. A small measurement error, incorrect blade selection, unstable slab support, poor machine setup, or careless material movement can turn an expensive granite, marble, quartz, porcelain, or sintered stone slab into scrap.
Many stone cutting errors do not actually begin at the cutting machine. They often start earlier in the production workflow, including slab storage, project measurement, cutting layout planning, material handling, equipment setup, tooling management, and production scheduling.
For stone factory owners and production managers, reducing mistakes therefore requires more than asking operators to “be careful.” The entire fabrication workflow should make correct operation easier, repeatable, measurable, and safer.
This guide explains 18 common fabrication mistakes, why they occur, the production risks they create, and how stone factories can build a more reliable process for reducing scrap, rework, damaged materials, and unnecessary production delays.
Why Fabrication Mistakes Are Expensive for Stone Factories
Stone fabrication is different from many manufacturing processes because the raw material can have relatively high value while offering limited opportunities for correction after a critical cut has been made.
If a countertop is cut too short, a sink opening is positioned incorrectly, a finished edge is damaged, or a fragile section breaks during handling, repairing the component may be difficult or impossible. In many cases, another section of slab must be processed.
Fabrication mistakes may create several direct and indirect costs:
- Loss of granite, marble, quartz, porcelain, or sintered stone material.
- Additional cutting, polishing, and finishing time.
- Extra machine operating hours.
- Higher tool consumption.
- Re-cutting and re-polishing work.
- Delayed production schedules.
- Additional packaging and transportation.
- Reduced production capacity.
- Customer complaints or installation problems.
- Additional handling and workplace safety exposure.
A factory processing large numbers of slabs does not need an extremely high defect rate for small recurring problems to become significant. This is why error prevention should be treated as a production-management system rather than only an operator responsibility.
Where Fabrication Errors Usually Begin
A useful way to understand fabrication mistakes is to divide the production process into several control stages.
| Workflow Stage | Typical Risk | Recommended Control |
|---|---|---|
| Slab storage | Impact damage, scratches, unnecessary movement | Organized rack layout and material identification |
| Measurement | Incorrect finished dimensions | Drawing, template, and specification verification |
| Slab inspection | Defects discovered after cutting | Pre-production visual and dimensional inspection |
| Cutting | Chipping, inaccurate cuts, tool damage | Correct tooling, support, cooling, and machine parameters |
| Handling | Cracks, edge damage, dropped material | Suitable lifting and transport equipment |
| Quality control | Errors discovered too late | Intermediate inspection checkpoints |
1. Starting Fabrication with Incorrect Measurements
One of the most serious fabrication mistakes is beginning production with inaccurate, incomplete, or outdated dimensions.
For countertops, vanity tops, wall panels, stair treads, islands, fireplace surrounds, and other custom stone products, cutting dimensions must represent the actual installation conditions.
A drawing may appear correct on a computer screen but still produce an incorrect finished product if wall angles, cabinet positions, appliance dimensions, overhangs, seams, or fixture positions were recorded incorrectly.
Common Measurement Problems
- Missing irregular wall conditions.
- Incorrect corner angles.
- Wrong sink or cooktop dimensions.
- Failure to account for countertop overhangs.
- Incorrect seam positioning.
- Using an outdated project drawing.
- Mixing metric and imperial dimensions.
- Incorrect data entry into CNC software.
- Failure to confirm appliance specifications.
A measurement verification step before production can prevent a very expensive mistake later. Project drawings, field measurements, digital templates, appliance specifications, and production files should be compared whenever the project requires them.
2. Failing to Inspect the Slab Before Cutting
Fabrication should not begin before the slab itself has been inspected.
Natural stone can contain veins, fissures, repaired areas, color variation, weak sections, resin-filled areas, scratches, or other characteristics that affect layout planning. Engineered quartz, porcelain, and sintered stone can also have pattern direction, surface imperfections, edge damage, or handling damage.
If these conditions are discovered only after cutting begins, the factory may lose the opportunity to reposition components.
Before Fabrication, Check:
- Overall slab dimensions.
- Material thickness.
- Surface scratches and chips.
- Cracks and natural fissures.
- Pattern and vein direction.
- Color consistency between slabs.
- Previous transportation or handling damage.
- Weak areas near planned cutouts.
Storage layout also affects inspection efficiency. When slabs are crowded, poorly identified, or repeatedly moved to reach other materials, inspection and production planning become more complicated.
Factories looking to improve this stage can review their stone slab rack layout and material flow to reduce unnecessary handling and improve access to inventory.
3. Poor Cutting Layout Planning
A professional cutting layout should be completed before the first production cut.
The goal is not simply to place the maximum number of components on one slab. The layout must balance material utilization with structural strength, visual appearance, production accessibility, and safe handling.
Layout planning should consider:
- Vein direction.
- Pattern matching between sections.
- Finished edge locations.
- Sink and cooktop openings.
- Seam positions.
- Weak or repaired areas.
- Required cutting allowance.
- Tool access.
- Handling space between components.
A layout that saves a small amount of material but produces difficult-to-handle or structurally weak components may create larger losses later in fabrication or installation.
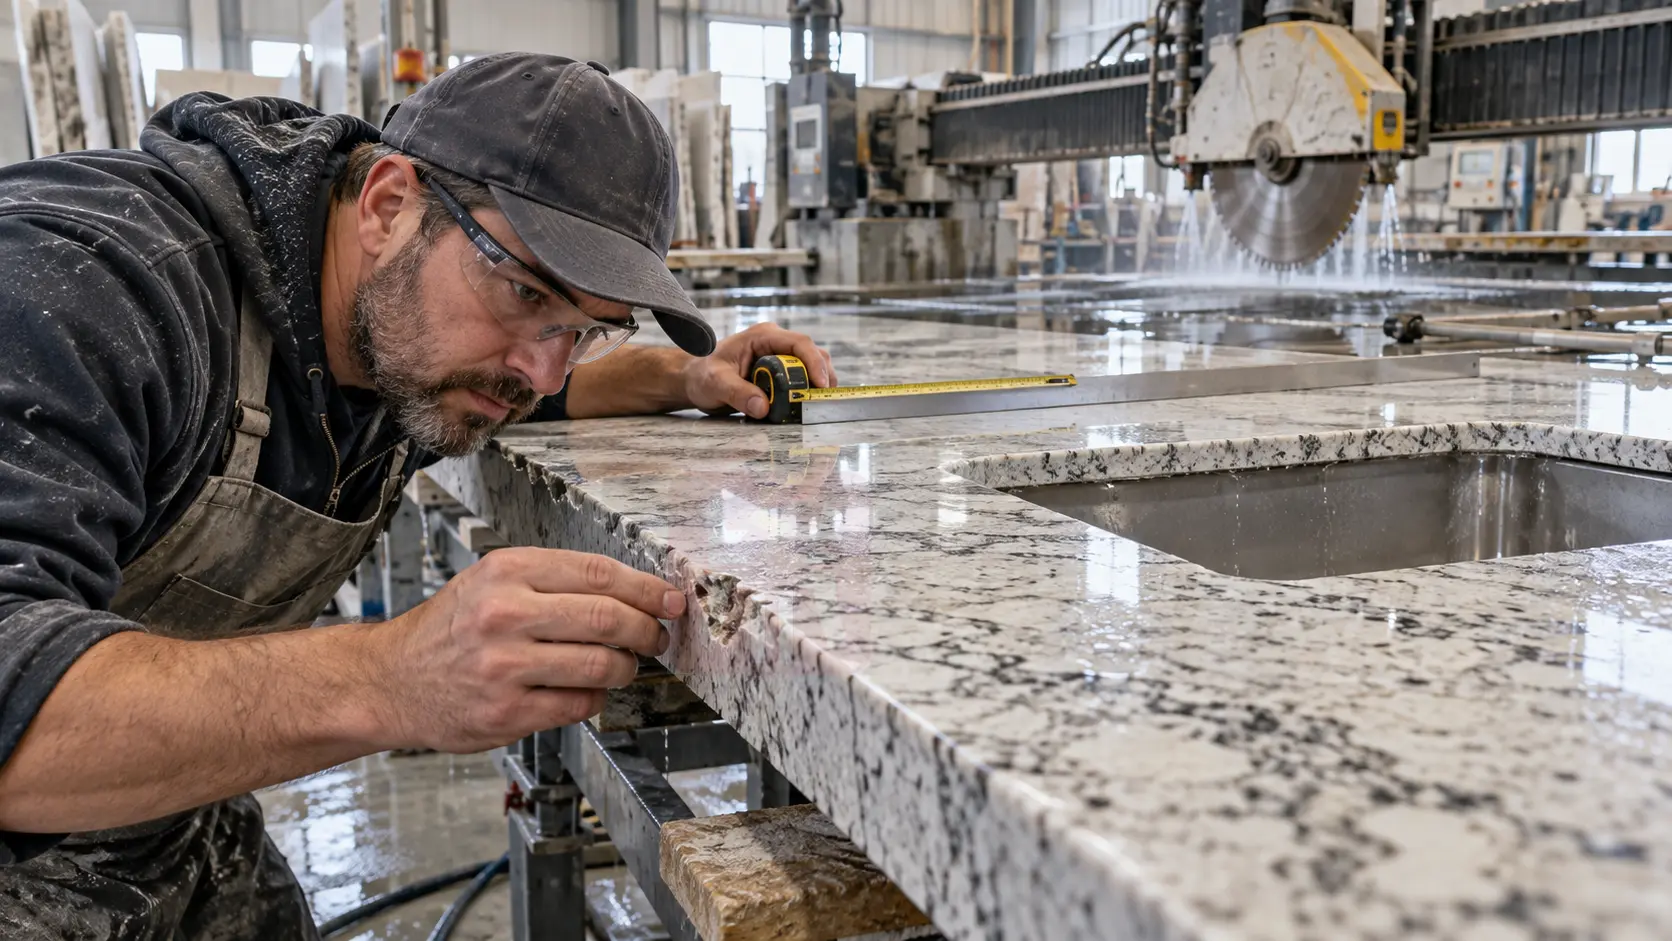
Stone cutting errors including chipped edges and incorrect cuts during slab fabrication
4. Using the Wrong Blade or Cutting Tool
Tool selection has a direct influence on cutting quality. Using an unsuitable diamond blade, drill bit, grinding wheel, router tool, or polishing pad can create multiple stone cutting errors.
Granite, marble, quartz, porcelain, and sintered stone do not behave exactly the same during processing. Tool selection should therefore follow the material, machine, cutting operation, and tool manufacturer’s recommendations.
Incorrect Tool Selection Can Cause:
- Edge chipping.
- Premature tool wear.
- Slow cutting performance.
- Excessive heat.
- Uneven cuts.
- Surface damage.
- Cracking near drilled or cut openings.
Factories processing several material types should clearly identify and organize tooling to reduce accidental misuse.
For a broader review of equipment used during stone processing, see this guide to essential stone fabrication tools.
5. Cutting Too Fast
Increasing machine feed speed may appear to improve productivity, but an aggressive cutting setup can create more rework than actual time savings.
Excessive speed may contribute to chipped edges, blade deflection, vibration, poor dimensional accuracy, overheating, premature tool wear, or inconsistent surface quality.
The correct operating parameters depend on several factors, including:
- Material type.
- Material thickness.
- Blade specification.
- Blade condition.
- Machine rigidity.
- Cooling conditions.
- Cut depth.
- Manufacturer recommendations.
The objective should be stable production quality rather than maximum theoretical feed speed.
6. Inadequate Water Cooling and Dust Control
Many cutting, grinding, drilling, and polishing operations use water for cooling, lubrication, debris removal, and dust suppression.
Insufficient or poorly directed water flow can affect both cutting performance and workplace conditions.
Potential Problems Include:
- Overheated diamond tools.
- Reduced blade life.
- Burning or discoloration.
- Increased edge chipping.
- Reduced polishing quality.
- Higher airborne dust generation.
Water nozzles, pumps, hoses, filters, and drainage systems should be inspected regularly. Operators should also follow applicable dust-control procedures and equipment instructions for the materials being processed.
Slurry should be managed so that wet fabrication does not create slippery floors, blocked drainage, or interference with surrounding machinery.
7. Poor Slab Support During Cutting
A large slab must remain stable and properly supported throughout the cutting operation.
Unsupported sections can move, flex, vibrate, or suddenly separate as the cut progresses. The problem becomes especially important when producing narrow strips, large islands, sink openings, unusual shapes, and components with narrow sections.
Poor support can contribute to:
- Unexpected material movement.
- Cracks around cut lines.
- Broken countertop sections.
- Blade binding.
- Dimensional inaccuracies.
The fabrication table should be stable, level, and suitable for the material dimensions. Offcuts should also be supported before the final cut completely separates them from the main slab.
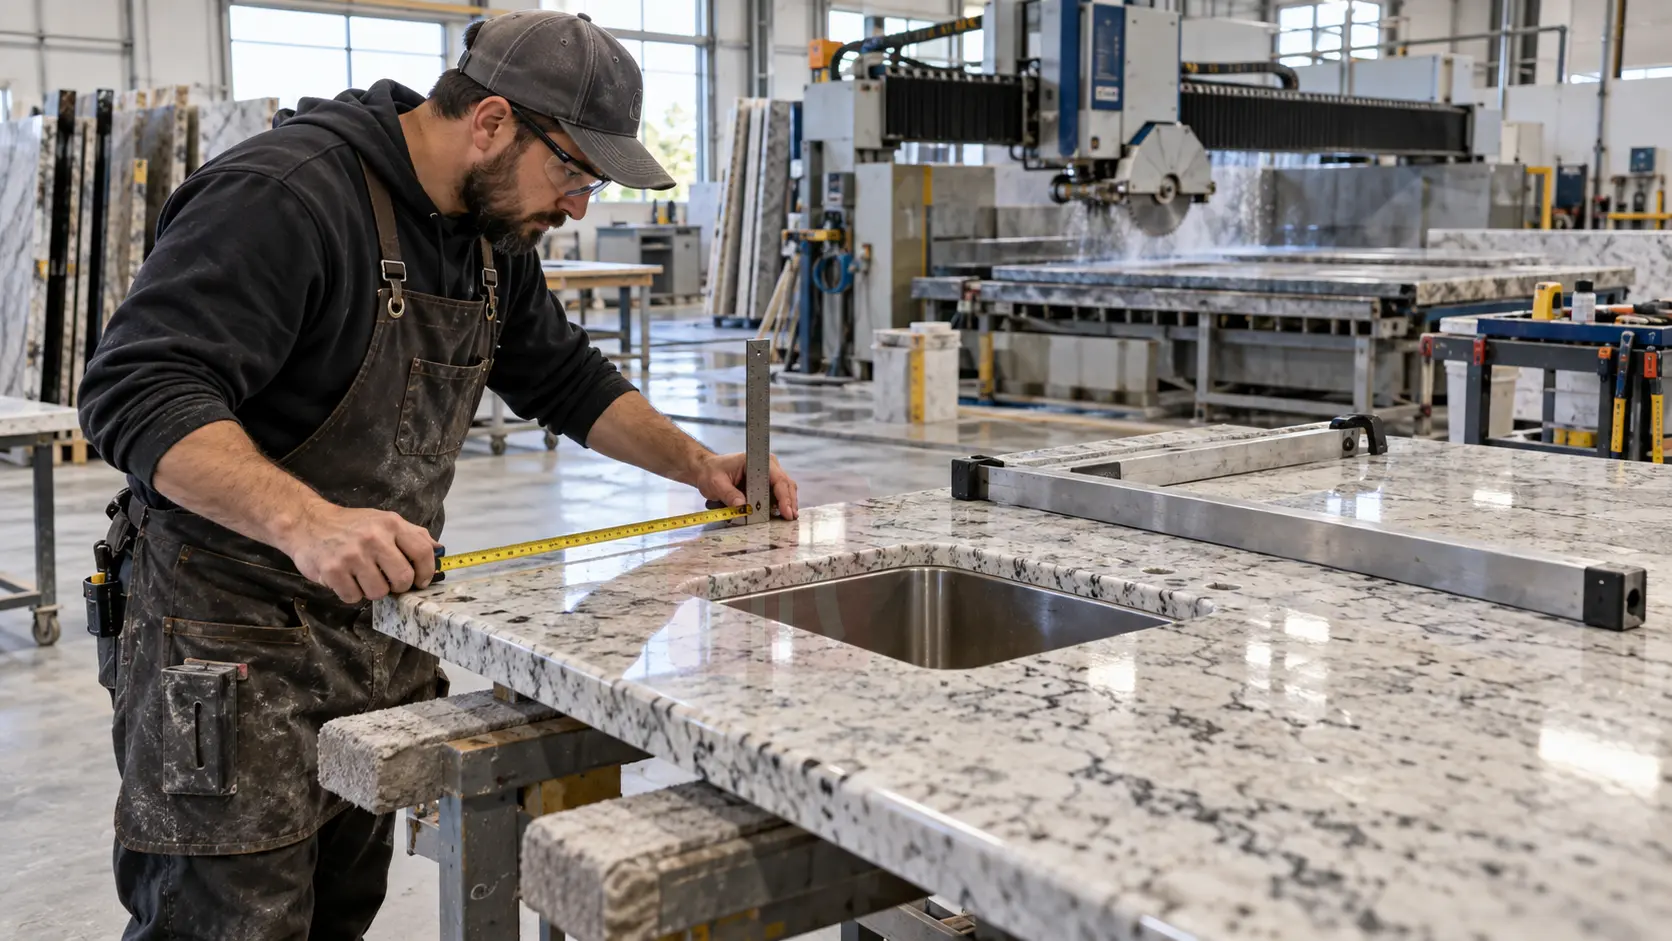
Stone fabrication quality control inspection for cutting errors and edge defects
8. Creating Sharp Internal Corners
Internal corners can become stress-concentration areas in stone components.
This is particularly important around sink openings, cooktop openings, inside corners, fixture openings, and narrow notches.
Where the design and material system permit, using an appropriate corner radius rather than an extremely sharp internal corner can help distribute stress more gradually.
The exact fabrication method should follow the material supplier’s technical guidance, project design, equipment capability, and applicable fabrication requirements.
9. Placing Cutouts Too Close to Finished Edges
Another common fabrication mistake is leaving a narrow section of material between an opening and the finished edge.
Thin rails around sink or cooktop openings can become particularly vulnerable during lifting, edge finishing, transportation, and installation.
Before cutting, fabricators should evaluate the remaining material around:
- Sinks.
- Cooktops.
- Faucet holes.
- Electrical openings.
- Fixture cutouts.
If a design creates a fragile area, additional temporary support or a revised handling method may be necessary during processing and transportation.
10. Ignoring Tool Wear
Diamond tools gradually change during operation. A worn blade or polishing tool may continue functioning while slowly producing poorer results.
Common warning signs include:
- Slower cutting.
- Increasing edge chips.
- Higher vibration.
- Longer polishing time.
- Uneven edge profiles.
- Inconsistent drilled-hole dimensions.
Instead of waiting until a tool completely fails, factories can establish inspection and replacement criteria based on machine hours, processed material, observed cutting quality, and manufacturer guidance.
11. Poor Machine Calibration
A perfectly prepared digital cutting file cannot compensate for an incorrectly calibrated machine.
Bridge saws, CNC machines, waterjets, edge polishers, drilling equipment, and other precision equipment require periodic inspection and calibration.
Calibration problems may produce:
- Incorrect dimensions.
- Out-of-square components.
- Misaligned openings.
- Incorrect drilling positions.
- Uneven edge profiles.
- Poor seam alignment.
Maintenance and calibration records help factories identify whether recurring production problems are related to tooling, machine condition, programming, or operator setup.
12. Selecting Equipment Only by Purchase Price
The lowest purchase price does not automatically create the lowest production cost.
Stone machinery and fabrication equipment should be evaluated according to the actual factory application.
Important considerations include processing accuracy, production volume, material compatibility, equipment rigidity, service requirements, spare parts availability, tooling costs, operator training, maintenance requirements, and expected service life.
Factories comparing machinery from different manufacturing regions can use this stone equipment comparison between China and Europe as a framework for reviewing technology, customization, support, acquisition cost, and long-term operating requirements.
Total Cost Matters More Than Purchase Price Alone
A more useful equipment comparison considers total operating cost rather than only the quotation.
A simple evaluation can include:
Total Ownership Cost = Purchase Cost + Installation + Tooling + Maintenance + Spare Parts + Training + Downtime Cost + Operating Cost
This does not mean the most expensive machine is automatically better. It means the equipment should be selected according to the work it must perform.
13. Unsafe or Inefficient Slab Storage
Some fabrication mistakes begin before the slab ever reaches the bridge saw or CNC machine.
Slabs stored on unsuitable racks or repeatedly moved to reach other inventory may develop edge damage, scratches, chips, or other handling problems.
Storage equipment should be selected according to slab dimensions, slab weight, loading method, aisle configuration, floor conditions, equipment access, and production sequence.
Reducing unnecessary slab movement is particularly important. Every additional handling step creates another opportunity for impact, contact, or operator error.
For practical storage considerations, review this guide to choosing stone slab racks for safe and efficient storage.
14. Improper Material Handling
A slab can be cut correctly and still be damaged during lifting, movement, or transfer between production stages.
Typical handling mistakes include:
- Using lifting equipment with unsuitable rated capacity.
- Selecting the wrong lifting method for the slab condition.
- Allowing finished edges to contact hard surfaces.
- Moving material too quickly.
- Failing to control the load during transport.
- Using lifting accessories that do not suit the load geometry or surface.
- Allowing personnel to enter unsafe areas around suspended or unstable slabs.
Equipment selection should consider material weight, dimensions, surface condition, load orientation, available headroom, lifting points, crane or forklift compatibility, and manufacturer instructions.
Factories reviewing this part of their workflow can refer to this guide on selecting suitable lifting equipment for a stone factory.
15. Poor Factory Layout
An inefficient workshop layout creates unnecessary material movement.
For example, slabs may travel from storage to cutting, back across the same aisle for CNC processing, across another area for polishing, and then return through the same traffic zone before packaging.
This type of workflow increases handling time as well as the opportunity for scratches, edge impacts, collisions, blocked work areas, operator fatigue, and production bottlenecks.
A more efficient production flow usually aims for a logical sequence such as:
Raw Slab Storage → Inspection → Cutting → CNC / Cutouts → Edge Processing → Polishing → Quality Inspection → Packing → Finished Product Storage
The exact layout will depend on the factory building, machinery, slab sizes, forklift routes, crane coverage, and production type.
Factories planning or reorganizing a facility can use this stone factory setup and workflow guide when reviewing equipment placement and material flow.
16. Skipping Intermediate Quality Checks
Waiting until the countertop reaches final inspection before checking important dimensions is another expensive mistake.
Quality checks should occur after critical fabrication stages so that problems are discovered before additional labor and machine time are added.
| Production Stage | Recommended Check |
|---|---|
| Before cutting | Confirm material, slab identity, dimensions, layout, pattern direction, and production file. |
| After primary cutting | Verify length, width, angles, orientation, and visible edge condition. |
| After cutouts | Check opening dimensions, position, corner geometry, and remaining material around the opening. |
| After edge processing | Inspect profile consistency, polish quality, chips, scratches, and seam edges. |
| Before packaging | Complete dimensional, visual, labeling, and project verification. |
17. Ignoring Small Stone Cutting Errors
Small defects should not automatically be treated as isolated incidents.
Repeated edge chipping, slightly inaccurate dimensions, unusual blade wear, vibration, polishing inconsistency, or recurring cracks may indicate a larger process problem.
Possible causes can include:
- Machine calibration.
- Blade condition.
- Incorrect feed parameters.
- Poor slab support.
- Cooling problems.
- Material variation.
- Operator setup.
Factories can create a simple defect log containing the material, machine, tooling, operator, defect type, suspected cause, corrective action, and final result.
Over time, recurring stone cutting errors can reveal which parts of the production system require the most attention.
18. Poor Packaging of Finished Stone Products
Fabrication is not complete when cutting and polishing end.
A correctly fabricated countertop can still be damaged during temporary storage, loading, transportation, unloading, or installation.
Finished edges and narrow areas around openings often require particular protection.
A suitable packaging and transport system should help prevent:
- Stone-to-stone contact.
- Finished-edge impacts.
- Uncontrolled movement during transport.
- Surface scratching.
- Concentrated pressure on fragile sections.
- Damage during loading and unloading.
Packaging should also be compatible with the lifting and unloading method expected at the destination.
Common Fabrication Mistakes and Their Solutions
| Fabrication Mistake | Possible Result | Recommended Action |
|---|---|---|
| Incorrect measurements | Poor fit or remake | Verify drawings, templates, appliance data, and dimensions before production. |
| Poor slab inspection | Defects positioned in critical areas | Inspect surfaces, veins, fissures, pattern direction, and damage before layout. |
| Wrong cutting tool | Chipping, slow cutting, excessive tool wear | Match tooling to material, machine, and operation. |
| Excessive cutting speed | Poor edge quality and dimensional errors | Use stable cutting parameters appropriate for the material and tool. |
| Poor slab support | Cracking or broken components | Provide stable support throughout cutting and separation. |
| Sharp internal corners | Stress concentration | Use suitable corner geometry where the design and material allow. |
| Worn tooling | Poor finish and inconsistent processing | Establish tooling inspection and replacement criteria. |
| Unsafe handling | Broken slabs, edge damage, safety exposure | Match lifting, transport, and storage equipment to the load. |
| No intermediate inspection | Errors discovered after additional work | Create quality checkpoints at critical stages. |
If You See This Problem, What Should You Check First?
Production defects often provide clues about their underlying cause. Instead of immediately changing several machine parameters at the same time, factories can begin with a structured diagnostic process.
| Observed Problem | Check First |
|---|---|
| Increasing edge chipping | Blade condition, feed parameters, water delivery, slab support |
| Dimensions gradually becoming inaccurate | Machine calibration, encoder or positioning system, production file |
| Cracks near openings | Corner geometry, remaining material width, slab condition, support method |
| Unexpected tool wear | Tool specification, operating parameters, cooling, material type |
| Damage after fabrication | Handling equipment, transport cart, storage method, packaging support |
How to Reduce Fabrication Mistakes in a Stone Factory
Reducing mistakes requires a production system that prevents errors before they become damaged slabs or rejected finished products.
1. Standardize Critical Processes
Create repeatable procedures for measurement review, slab identification, slab inspection, cutting setup, tooling selection, cutout fabrication, edge processing, inspection, material handling, and packaging.
Standardization helps reduce variation between operators and shifts.
2. Maintain Equipment Before Accuracy Begins to Decline
Machine accuracy depends on mechanical condition, calibration, tooling, cooling, alignment, and operator setup.
Preventive maintenance should therefore be planned rather than performed only after defective products appear.
3. Improve Material Flow
Every unnecessary slab movement introduces additional handling time and another opportunity for damage.
Storage racks, fabrication tables, cutting equipment, finishing stations, inspection areas, and packing zones should be organized around a logical production sequence whenever the building allows it.
4. Match Handling Equipment to the Material
Material handling is part of fabrication quality control.
Depending on the process, factories may use slab racks, A-frame systems, transport carts, lifting clamps, vacuum lifters, forklift attachments, lifting beams, or other purpose-designed equipment.
The correct solution depends on load weight, dimensions, surface condition, available lifting machinery, travel distance, orientation, and factory layout.
5. Track Production Errors
Factories should classify recurring defects rather than relying only on informal operator feedback.
If one type of defect repeatedly appears on the same machine, material, shift, tool, or processing stage, management can concentrate corrective action where it is most useful.
6. Train Operators Around Causes, Not Only Instructions
An operator who understands why blade condition, cutting speed, slab support, coolant delivery, and inspection steps matter is more likely to recognize an abnormal condition before it becomes a serious defect.
A Simple Fabrication Error Prevention Framework
Factories do not necessarily need a complicated management system to improve immediately. A practical workflow can begin with eight control points:
Measure → Inspect → Plan → Support → Process → Check → Handle → Pack
At each stage, the production team should ask one question: What could make this component unusable at the next stage?
This approach helps move quality control upstream. Instead of discovering mistakes only when the finished countertop reaches packaging, problems are identified while they may still be corrected.
Which Improvements Should a Factory Prioritize First?
Not every stone factory has the same bottleneck. The first improvement should target the area producing the most frequent or expensive errors.
- If dimensions are frequently wrong: review measuring, templating, drawing control, CNC data entry, and machine calibration.
- If edges chip during cutting: review tool condition, blade selection, cutting parameters, cooling, and slab support.
- If slabs break during movement: review lifting equipment, transport method, rack configuration, load capacity, and operator procedure.
- If production is slow despite good machines: review factory layout, material flow, tool changes, slab access, and intermediate handling.
- If defects are discovered only before shipping: introduce intermediate quality-control checkpoints.
- If the same defect repeatedly returns: create an error log and investigate the common cause rather than repeatedly repairing the symptom.
Reducing Errors Is Also a Factory Capacity Strategy
Many factories think about increasing capacity mainly by purchasing faster machinery. However, production output is also affected by rework, repeated material movement, waiting time, machine downtime, missing tools, damaged slabs, and quality failures.
Reducing fabrication mistakes can therefore improve effective capacity even without increasing nominal machine speed.
For example, if a bridge saw completes a cut quickly but operators later spend additional time correcting chipped edges, replacing broken components, locating replacement slabs, or remaking incorrectly sized parts, the factory has not truly gained productive capacity.
The objective should be consistent first-pass quality combined with efficient material movement.
What Factory Managers Should Monitor
Useful production indicators do not need to be complicated. Depending on the operation, a factory may track:
- Number of remakes.
- Reasons for rejected components.
- Material loss by defect type.
- Machine downtime caused by tooling or calibration.
- Handling damage.
- Late-discovered measurement errors.
- Packaging or transportation damage.
- Recurring customer complaints.
The purpose is not simply to create more paperwork. The information should help management identify which process is causing the highest-value losses and where corrective action should begin.
Before Buying New Equipment, Identify the Real Problem
New machinery can solve certain production problems, but equipment should not be used as a substitute for process diagnosis.
Before purchasing a new saw, fabrication table, slab rack, lifting attachment, or transport system, define the actual bottleneck.
Ask whether the main problem is:
- Cutting accuracy.
- Production speed.
- Slab access.
- Material handling.
- Limited floor space.
- Unsafe lifting.
- Tooling performance.
- Machine downtime.
- Quality inspection.
Once the cause is clear, equipment can be selected according to the specific production requirement rather than only by price or specification sheet.
Practical Checklist Before the First Cut
- Confirm project number and correct slab.
- Verify finished dimensions.
- Review drawing or digital template.
- Check appliance and fixture dimensions.
- Inspect slab condition.
- Confirm pattern and vein direction.
- Review component layout.
- Check blade or tooling condition.
- Confirm machine calibration where required.
- Verify water or cooling delivery.
- Confirm slab and offcut support.
- Prepare the next handling step before cutting begins.
A short pre-cut verification can prevent a long chain of rework later.
Soft CTA: Improve the Workflow Before Adding More Production Pressure
If your factory is experiencing repeated slab damage, unnecessary material movement, cutting defects, broken countertop sections, or frequent rework, begin by mapping the full workflow from slab storage to finished-product loading.
Record the slab dimensions and weights you normally process, the equipment currently used, aisle conditions, lifting methods, cutting workflow, and the stages where damage or delays most often occur.
This information makes it much easier to determine whether the real solution involves better storage, a more suitable fabrication table, improved slab transport, different lifting equipment, revised factory layout, or changes to the cutting process itself.
References and Safety Resources
The following resources can be used together with equipment manufacturer instructions, material supplier guidance, and local workplace requirements when developing stone-fabrication procedures:
- Occupational Safety and Health Administration, 29 CFR 1910.176, Handling Materials, General.
- Occupational Safety and Health Administration, Safety and Health Information Bulletin: Hazards of Transporting, Unloading, Storing and Handling Granite, Marble and Stone Slabs.
- Occupational Safety and Health Administration, 29 CFR 1910.1053, Respirable Crystalline Silica.
- Natural Stone Institute safety and fabrication resources.
- Machine, tooling, lifting-equipment, and material manufacturers’ operating and technical instructions.
Nota final / Conclusões práticas
Most fabrication mistakes are not isolated accidents. They usually reveal a weakness somewhere in the production system. Inaccurate measurements, poor slab inspection, unsuitable tooling, unstable support, incorrect machine settings, inefficient material flow, unsafe handling, and weak quality-control procedures can all contribute to recurring stone cutting errors. The most effective stone factories treat fabrication quality as a complete workflow. By controlling the process from slab storage and measurement through cutting, inspection, handling, and packaging, factories can reduce scrap, rework, avoidable damage, and production disruption while creating more consistent finished products.
Frequently Asked Questions About Fabrication Mistakes
1. What are the most common fabrication mistakes in stone processing?
Os erros comuns de fabricação incluem medições incorretas, inspeção deficiente das lajes, layouts de corte ineficientes, ferramentas de corte inadequadas, velocidade excessiva de corte, resfriamento insuficiente, suporte inadequado para as lajes, recortes imprecisos, ferramentas desgastadas, problemas de calibração das máquinas, manuseio inseguro, controle de qualidade fraco e embalagem inadequada.
2. What causes stone cutting errors?
Erros de corte em pedra podem ser causados por lâminas desgastadas, ferramentas inadequadas, parâmetros de corte incorretos, resfriamento insuficiente, suporte inadequado do material, arquivos CNC imprecisos, calibração deficiente da máquina, defeitos no material ou configuração incorreta pelo operador.
3. How can a stone factory reduce material waste?
Uma fábrica pode reduzir o desperdício de materiais melhorando a inspeção das placas, otimizando os layouts de corte, verificando as medidas antes da produção, realizando a manutenção de máquinas e ferramentas, controlando os parâmetros de corte, aprimorando o manuseio dos materiais e registrando defeitos recorrentes na produção.
4. Why does slab handling affect fabrication quality?
A pedra pode ser danificada antes ou depois do corte se for armazenada, levantada, transferida ou transportada de forma incorreta. Estantes adequadas para armazenamento, carrinhos de transporte, equipamentos de elevação e suportes protetores podem reduzir movimentos descontrolados, arranhões, impactos nas bordas, rachaduras e quebras.
5. How often should fabrication equipment be inspected?
A frequência de inspeção depende do tipo de máquina, das horas de operação, do volume de produção, dos materiais processados, das condições de trabalho e das recomendações do fabricante. A inspeção preventiva e a calibração devem ser agendadas, em vez de esperar até que os produtos acabados apresentem defeitos visíveis.
6. How can I identify the cause of repeated edge chipping?
Comece verificando a condição da lâmina, a adequação da lâmina ao material, a velocidade de corte, a entrega de água, a vibração da máquina e o suporte da laje. Se o problema persistir, revise a calibração da máquina e verifique se o próprio material apresenta defeitos ou áreas fracas.
7. Is buying a more expensive machine the best way to reduce fabrication mistakes?
Not necessarily. Equipment should match the factory’s actual production requirements. Poor measurements, incorrect tooling, weak slab support, inefficient workflow, or unsafe handling will not automatically disappear after buying a more expensive machine. Identify the cause of the problem before selecting new equipment.
8. What is the best way to prevent fabrication errors before cutting?
Utilize um processo de verificação de pré-produção que confirme a laje correta, as dimensões, o desenho do projeto, a direção do padrão, o layout de corte, as condições das ferramentas, a configuração da máquina, o sistema de resfriamento, o suporte da laje e a próxima etapa de manuseio antes que o primeiro corte seja realizado.

Henrique
Olá, sou o autor deste post, e estou neste sector há mais de 16 anos. Se precisar de um serviço OEM&ODM para ferramentas de pedra, não hesite em colocar-me quaisquer questões.