効率的に仕事をこなす




A successful stone factory setup depends on more than purchasing cutting and polishing machines. Factory layout, slab storage, material handling, processing stations, quality control, waste management, and internal logistics must work as one system. This guide explains how to build an efficient fabrication workflow for granite, marble, quartz, and other slab materials while reducing unnecessary handling, slab damage, and production bottlenecks.
Factory Setup Guide for Stone Processing
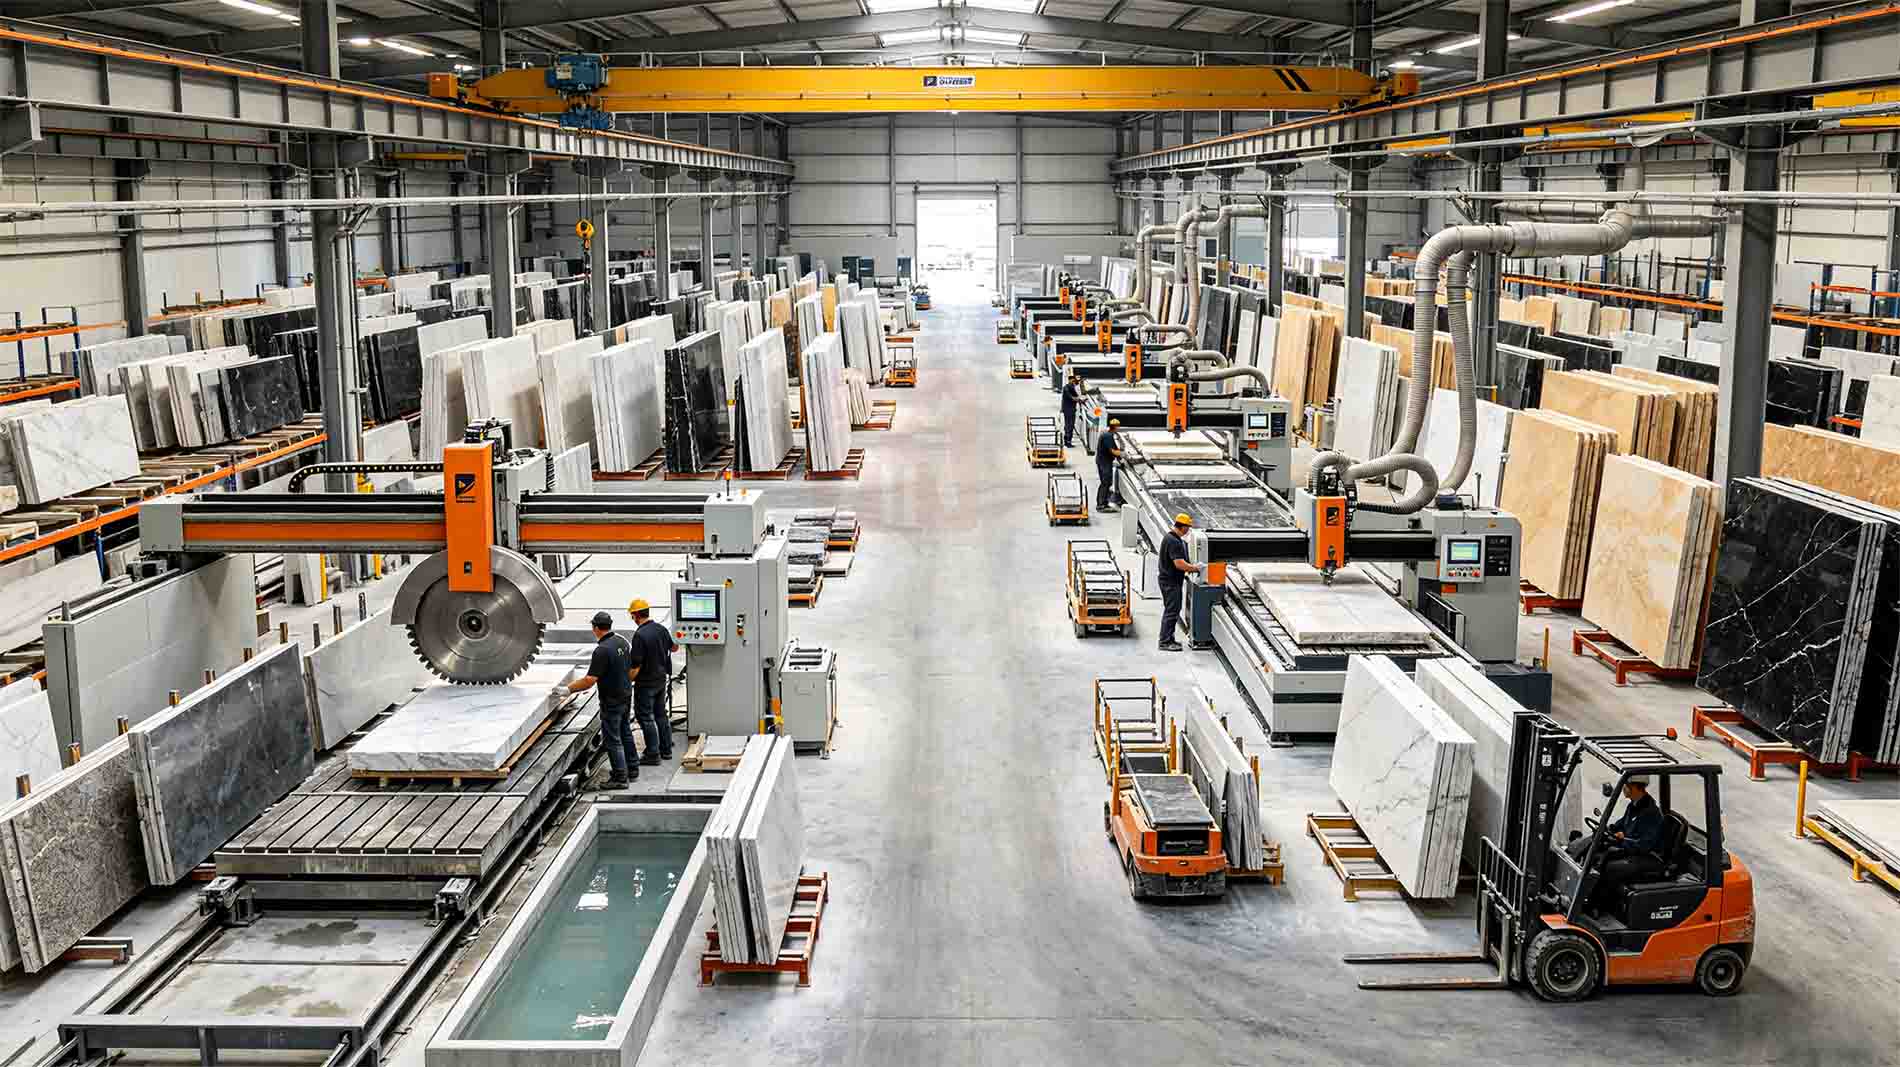
Factory stone materials
A well-planned stone factory setup creates a continuous path from incoming raw slabs to finished countertops, panels, tiles, or custom stone components. Cutting equipment may perform the main processing work, but the overall productivity of a factory also depends on how efficiently slabs are stored, moved, inspected, processed, and prepared for shipment.
For this reason, a modern fabrication workflow should be designed as an integrated material flow rather than a collection of individual machines. Every unnecessary transfer, sharp turn, blocked aisle, or poorly positioned storage area can increase handling time and expose valuable stone to additional risk.
Whether a company is establishing a new stone processing facility or upgrading an existing workshop, planning the layout around material movement can help improve throughput, workplace organization, and long-term scalability.
What Should a Stone Processing Factory Include?
The exact equipment depends on the products being manufactured, but most stone processing facilities contain several functional zones.
- Raw slab receiving and inspection area
- Slab storage system
- Primary cutting area
- CNC or secondary fabrication area
- Edge processing and polishing stations
- Quality control and dry-fit area
- Finished-product storage area
- Packing and dispatch zone
- Stone waste collection area
- Internal material transport routes
The important point is not simply having these areas. Their positions should follow the actual production sequence so that slabs move forward through the factory instead of repeatedly crossing the same spac
Recommended Stone Factory Workflow
| Production Stage | Main Activity | Key Setup Priority |
|---|---|---|
| Receiving | Unload and inspect raw slabs | Safe access and identification |
| Storage | Organize slabs before production | Capacity and retrieval efficiency |
| Cutting | Primary sizing and shaping | Precision and material flow |
| Fabrication | CNC, drilling and edge work | Stable work support |
| Finishing | Polishing and inspection | Quality consistency |
| Dispatch | Pack, stage and load products | Damage prevention |
1. Plan Material Flow Before Positioning Machines
One of the biggest mistakes in factory planning is deciding where machines will stand before mapping how material will travel between them. Large stone slabs are difficult to maneuver, so every transfer should be considered during the initial layout.
Start by drawing the complete path of a typical slab:
- Truck or container to receiving area
- Receiving area to raw slab storage
- Storage to cutting machine
- Cutting to fabrication station
- Fabrication to finishing and inspection
- Inspection to finished-product storage
- Finished storage to packing and dispatch
The ideal arrangement minimizes backtracking and unnecessary crossings between forklifts, transport carts, operators, and stationary machinery.
Internal transport deserves particular attention because it can become an overlooked production constraint. The analysis of slab transport bottlenecks in stone workshops shows why improving movement between production stages can be just as important as increasing machine capacity.
2. Design an Efficient Slab Receiving and Storage Area
Raw material handling begins as soon as slabs enter the facility. The receiving zone should provide sufficient clearance for unloading equipment and allow operators to inspect materials before they enter production.
A practical receiving procedure normally includes checking slab quantity, dimensions, surface condition, identification numbers, and visible damage. After inspection, slabs should be transferred to a suitable storage location rather than remaining in unloading areas where they can interfere with traffic.
Storage capacity should also account for future growth. A facility that works comfortably at today’s inventory level may become congested if production increases without additional storage planning.
3. Separate Cutting, Fabrication, and Finishing Zones
Stone processing produces water, slurry, dust, noise, and offcuts. Separating major operations into clearly defined zones helps maintain a more organized production environment.
Primary Cutting Zone
Bridge saws, sawjets, and other cutting machines require enough surrounding space for loading slabs and removing cut components. The area should also provide a direct connection to raw material storage whenever possible.
Secondary Fabrication Zone
CNC machining, sink cutouts, drilling, profiling, and manual fabrication should be arranged so that operators can move partially processed pieces without repeatedly crossing major traffic routes.
Finishing and Inspection Zone
Finished surfaces require more careful handling. Polishing, final inspection, and dry fitting should therefore take place in an area where completed pieces are less likely to be exposed to unnecessary traffic or rough material handling.
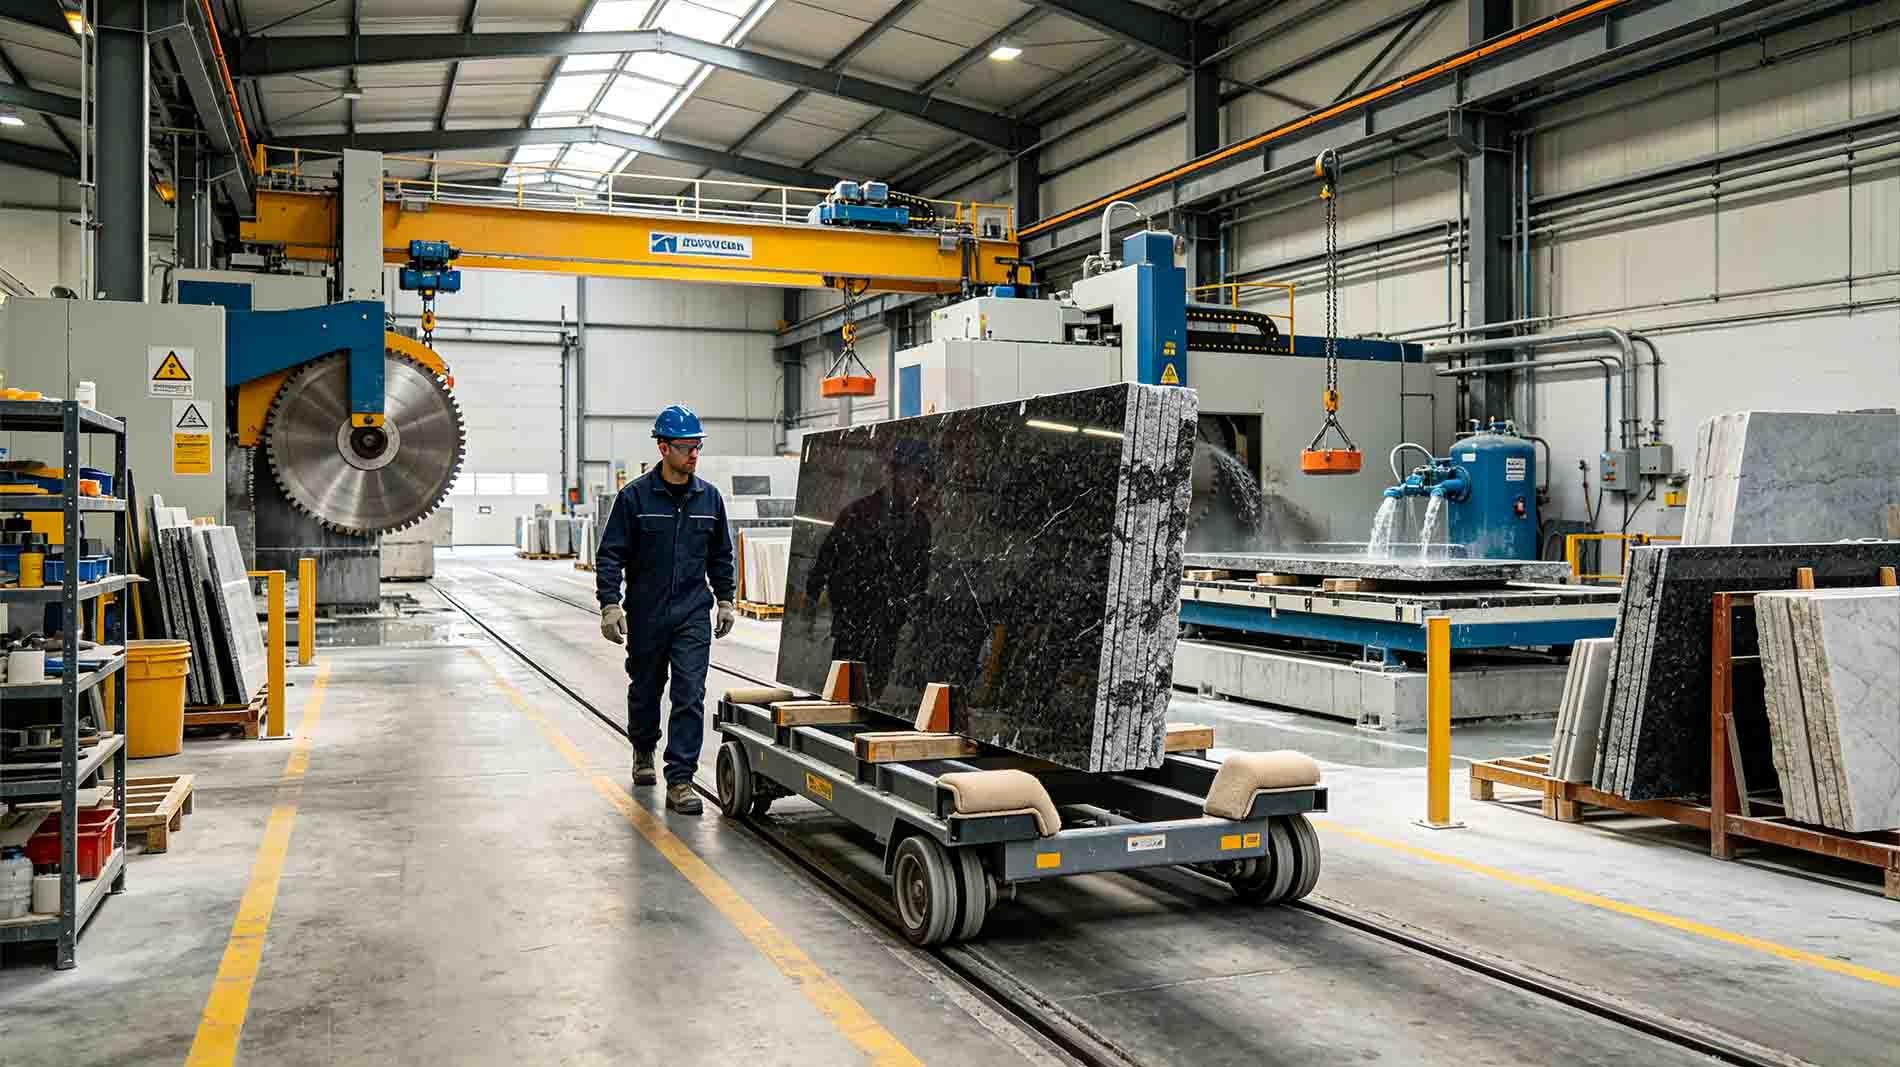
Sheet material transportation
4. Build Internal Slab Transport into the Fabrication Workflow
A factory may have fast cutting and polishing equipment but still lose considerable time if workers struggle to move slabs and finished pieces between stations. Internal transport should therefore be treated as production equipment rather than an afterthought.
Different factories require different cart configurations depending on load capacity, aisle width, floor condition, slab dimensions, and travel distance. Before purchasing equipment, factories can review how to select the right slab transport cart for stone factories and match the cart design to actual production requirements.
For repeated transfers between fixed production stations, specialized designs can also improve control. For example, self-locking trolley systems for slab handling can support more controlled movement when the application requires stable positioning and frequent transfers.
5. Reduce Slab Damage Between Processing Stages
Damage does not occur only during cutting. Slabs and fabricated components can be chipped, scratched, cracked, or broken during internal movement.
Common causes include:
- Sudden starts or stops while transporting slabs
- Insufficient support underneath finished pieces
- Contact between polished surfaces
- Incorrect load positioning
- Congested transport routes
- Excessive manual handling
These losses are easy to underestimate because small incidents may be recorded as rework rather than logistics costs. A deeper review of the hidden costs of slab damage during transportation explains why material handling should be included when evaluating overall factory efficiency.
6. Choose Transport Equipment According to the Material
Not every product follows the same handling route. Large raw slabs, cut countertops, glass panels, quartz pieces, and finished stone components can require different support structures.
Double-sided A-frame carts are useful when materials need vertical support during internal movement. A practical example is a 2000 kg double-sided A-frame transport cart, which illustrates how a mobile support structure can combine temporary holding and transportation functions.
Equipment selection should consider more than maximum capacity. Wheel type, maneuverability, frame dimensions, loading surface, floor condition, and compatibility with upstream and downstream equipment can all affect daily performance.
7. Establish Safe Traffic Routes
A good stone factory setup should separate people and moving loads wherever practical. Forklifts, slab carts, lifting devices, and employees should not compete for the same narrow pathways.
Factory planners should identify:
- Main forklift routes
- Pedestrian walkways
- Loading and unloading zones
- Temporary slab staging areas
- Emergency exits
- Machine maintenance access
Clear routes can reduce unnecessary stopping and improve visibility. Floor markings, signage, mirrors at blind corners, and designated staging areas can further improve organization.
8. Connect Material Handling with Production Scheduling
Production scheduling is often focused on machine availability, but a job is not truly ready for processing unless the correct slab can reach the correct machine at the required time.
Factories can improve coordination by linking job identification, slab location, production priority, and transport tasks. Even a simple system that clearly identifies where each slab should move next can reduce searching and waiting.
The goal is to create a predictable flow rather than relying on operators to solve transportation problems after each processing stage.
9. Create a Dedicated Finished-Product and Dispatch Zone
Once fabrication is complete, finished pieces should be moved away from heavy processing areas. Countertops and polished components are particularly vulnerable because cutouts, narrow sections, and finished edges can make them more fragile than raw slabs.
A dedicated dispatch zone allows products to be inspected, organized by project, protected, and prepared for loading without interfering with active fabrication.
Improving the connection between production and dispatch is part of a broader logistics strategy. This guide to improving stone logistics with safe slab transport provides additional insight into how appropriate handling equipment can support smoother movement throughout the facility.
10. Plan for Stone Waste and Housekeeping
Stone processing creates broken pieces, narrow offcuts, slurry, packaging materials, and other waste. If waste handling is not incorporated into the original layout, disposal activities can interfere with production routes.
Locate waste collection points close enough to production areas for convenient disposal but away from primary material traffic. Regular removal schedules help prevent waste from accumulating around machines and transport routes.
Good housekeeping also makes it easier to identify floor hazards and maintain clear access around equipment.
Stone Factory Setup Checklist
| Area | Check Before Operation |
|---|---|
| Receiving | Adequate unloading clearance and inspection space |
| Slab Storage | Suitable capacity, access, and organization |
| Processing | Logical machine sequence and working clearance |
| Transport | Suitable carts, clear aisles, and defined routes |
| Quality Control | Dedicated inspection and dry-fit space |
| Dispatch | Protected staging and packing area |
| Waste | Defined collection and removal process |
How to Improve an Existing Stone Factory
An existing workshop does not necessarily require a complete rebuild. Improvements can begin by observing the current fabrication workflow and identifying where material stops, waits, reverses direction, or requires repeated handling.
A practical improvement process is:
- Map the current slab movement route.
- Record repeated transfers and waiting points.
- Identify congested aisles and staging areas.
- Review whether transport equipment matches current loads.
- Move frequently connected processes closer together where possible.
- Create dedicated storage and dispatch locations.
- Measure results after layout changes.
Rather than focusing only on machine speed, factories should evaluate the total time required for a slab to travel from receiving to dispatch. This provides a more realistic picture of production performance.
最終ノート/実践的な収穫
An efficient stone processing factory should be designed around material flow, not simply around individual machines. Cutting capacity has limited value when slabs wait for transport, aisles are congested, or finished pieces require excessive handling. The strongest stone factory setup connects receiving, storage, fabrication, internal transportation, quality control, and dispatch into one coordinated system. For new facilities, planning these relationships before installing equipment can prevent expensive layout problems. For existing factories, analyzing transport bottlenecks and unnecessary slab movements is often one of the most practical starting points for improving the fabrication workflow.
よくある質問
1. What is the most important factor in a stone factory setup?
材料の流れは最も重要な要素の一つです。保管、切断、加工、仕上げ、輸送、出荷の各エリアは、スラブが生産工程を最小限の後戻りと無駄な取り扱いなしに移動できるよう配置する必要があります。
2. What equipment is needed for a stone processing factory?
要件は製品ごとに異なりますが、一般的な施設ではスラブ保管システム、切断機、CNCまたは加工設備、研磨工具、作業台、リフティング設備、スラブ運搬カート、品質管理エリア、廃棄物処理システムなどが使用されます。
3. How can a factory improve its fabrication workflow?
施設内の材料の全行程をマッピングすることから始めましょう。待ち時間のポイント、繰り返し行われる搬送、混雑する経路、不要な移動を特定し、設備の配置や搬送方法を調整することで、より連続的な生産フローを実現しましょう。
4. Why are slab transport carts important in stone factories?
スラブ運搬カートは、重い生のスラブや加工済み部材を生産工程間で移動するのに役立ちます。適切に選ばれた設備を使用することで、手作業による取り扱いを減らし、移動効率を向上させ、内部輸送中の石材の損傷を防ぐことができます。
5. How should a growing stone factory plan for future expansion?
スラブ保管エリア、搬送通路、仮置き場、設備エリア、および発送エリアに追加の容量を確保します。モジュール式のレイアウトと明確に定義された物流経路により、設備を追加したり生産量を増やしたりする際に、工場全体を中断することなく容易に行えます。

ヘンリー
こんにちは、私はこの記事の著者です。石工具のOEM&ODMサービスが必要な場合は、お気軽にご質問ください。